

The project of purification and surplus heat recovery of flue gas from coal-burning boilers of Jinan Beijiao CHP
Project Background
Jinan Beijiao Thermal Power Co., Ltd. is affiliated to Jinan Heat and Power Co., Ltd., with main business in urban heat supply and concurrent business in power, steam and hot water supply. In 2015, Beijing Keyuan Ruineng Energy-saving Equipment Co., Ltd. implemented deep flue-gas purification and waste heat recovery on the coal-fired boilers of the plant, significantly reducing the exhaust temperature and using the recovered heat for heating supply, while cutting the emission of particles, sulfur oxides and nitrogen oxides — achieving energy saving, environmental protection and water saving at the same time. This is the first application of deep flue-gas waste heat recovery technology at a coal-fired power plant in the world.
On December 2, 2015, the State Council decided to fully implement ultra-low emission and energy-saving retrofits of coal-fired power plants. The flue gas from coal-fired boilers after wet desulfurization is about 52°C and carries a large amount of water vapor; its complex composition and strong corrosion cause many bottlenecks in heat recovery. The project successfully overcame these difficulties and achieved the multiple benefits of energy saving, emission reduction and water saving.
Process Flow
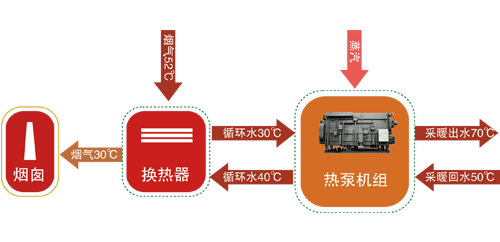
The flue gas from coal-fired combustion passes through wet desulfurization and then enters the heat exchanger, where the latent and sensible heat is deeply recovered and pollutant emissions are reduced, so that the boiler exhaust temperature drops significantly; the recovered heat is used to heat the network return water or for direct heat supply.
Technical Advantages
- Coal boiler exhaust temperature reduced to below 30°C;
- Coal boiler efficiency improved by more than 10%;
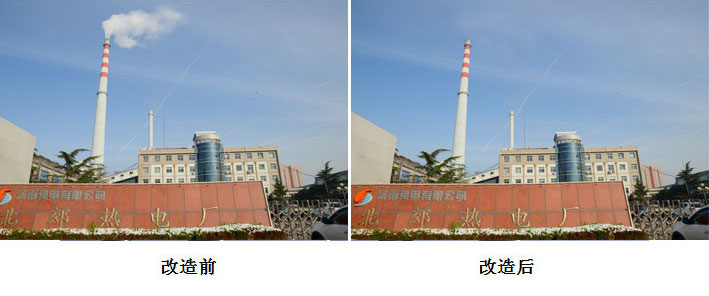
- Dust, NOx, SO2 and other pollutant emissions reduced, white plume eliminated;
- The unit can provide cooling in summer — one unit, two uses.